Quartz stone purification process
Brief Introduction to the Quartz Purification Process: Quartz purification involves a highly complex separation process that removes small or trace impurities from quartz to produce refined quartz sand or high-purity quartz sand (e.g., for electronic-grade products). In recent years, the main process for producing high-purity quartz sand in China is as follows: The raw silica ore is washed to remove sediment in a ore washer. After coarse crushing in a crusher, the qualified quartz material is placed in a roaster and roasted at 850°C-980°C for six hours. After roasting, the quartz material is quenched in clean water. After manual sorting to remove impurities, it is sent to a crusher for crushing and screening. The quartz sand that passes through the screen is then sent to a magnetic separator. After magnetic separation, the sand is soaked in a mixed acid tank containing HCl and HF for one week. The sand then undergoes flotation, dehydration, roasting, cooling, and packaging to produce high-purity quartz sand.
The specific steps of the quartz stone purification process are as follows:
1. Roughing: Removes visible impurities and foreign matter from various types of quartz ore;
2. Crushing: Uses a specialized crusher to crush the quartz ore into particles ranging from 1 to 20 mm in size;
3. Water Quenching: Rapidly cools the calcined quartz particles in cold water to remove internal bubbles, water marks, and some encapsulated impurities, thereby cracking the mineral. Quartz calcination and water quenching, also known as thermal cracking, involves the transformation of quartz's crystal form (α quartz → β quartz → β tridymite) during high-temperature calcination. This causes the crystal to expand in size and exacerbate existing defects. During water quenching, the crystal suddenly shrinks in size, rapidly increasing internal stress at the defects and causing the crystal to fracture at these locations. This cracking exposes inclusions and impurities from the original quartz's cracks to the particle surface, making them easily removed during acid treatment.
4. Pulverization: Wet or dry grinding is used to produce ultrafine quartz sand with a particle size of 5-50μm.
5. Magnetic Separation: High-gradient magnetic separation equipment with a magnetic field strength of 50-15,000 gauss is used to remove magnetic minerals such as limonite, hematite, mica, garnet, pyrite, and ilmenite. The process generally involves at least two stages of magnetic separation. The leading stage primarily removes strongly magnetic materials from the ore to prevent adverse effects on subsequent operations. The second stage primarily removes weakly and extremely weakly magnetic minerals. The leading stage typically uses a permanent high-magnetic drum magnetic separator with a magnetic field of approximately 6,000-8,000 gauss. The second stage typically uses a permanent high-gradient magnetic separator or an electromagnetic induction separator. The former is more popular in the market due to its lower energy consumption, lighter weight, higher magnetic field gradient, and relatively lower investment. Some believe that magnetic separation is solely responsible for reducing iron content, but this is not the case. Practice has proven that magnetic separation can, to a certain extent, reduce the content of impurities such as aluminum, potassium, and sodium. Furthermore, magnetic separation can remove impurities that cannot be removed by acid washing or flotation. Magnetic separation is an essential step in the production of high-purity quartz.
6. Classification: Using grading equipment, the raw materials are separated into various particle size ranges according to standards. In subsequent processing, these products are processed separately based on their particle size ranges. Grading equipment can be divided into screening machines and airflow classifiers. The choice of grading equipment depends on production volume and the required particle size range.
7. Calcination: Using a specialized roasting furnace, the raw quartz ore particles are roasted at 300°C-1500°C for 2-5 hours. Chlorination roasting is the primary method for removing quartz lattice impurities, and different chlorinating agents have significant differences in their interaction and effectiveness with lattice impurities. (Please contact us for more detailed information on specific results.)
8. Water Crushing: The calcined quartz particles are quickly cooled in room temperature hot water to dissolve the soluble substances produced by calcination. The water is then heated for 0.5-2 hours to increase the solubility of these soluble substances.
9. Flotation: A flotation agent is added to the quartz sand powder after water crushing to remove impurities with a specific gravity less than 1. This primarily removes non-magnetic impurities such as feldspar and pure muscovite.
10. Deionized Water Washing: Deionized water is used to wash away any remaining flotation agent and quartz. Impurities on the sand surface;
11. Drying: After washing with deionized water, the quartz sand is first air-dried (drying in the sun) to remove large amounts of water. It is then dried in specialized drying equipment and heated to 100-200°C.
12. Acid Leaching: The dried quartz sand is placed in an immersion tank. Under dry, high-temperature conditions, the acid used for leaching (sulfuric acid, hydrochloric acid, nitric acid, or hydrofluoric acid) is quickly added at a concentration of 5%-20%. Stirring is performed at a constant temperature of 30-100°C for 2-24 hours to remove trace metallic and non-metallic impurities from the fine quartz sand powder. Acid leaching is one of the important processes in the purification of high-purity quartz sand. It is a necessary process whether it is used to prepare quartz glass for electric light sources or quartz raw materials for photovoltaic and semiconductor devices. Acid leaching is mainly used to remove metal oxides and some silicate minerals soluble in acid, as well as trace impurities such as soluble aluminum and iron in the ore. After roasting, water quenching, sorting, and strong magnetic separation, most oxides and impurity minerals have been removed, but some oxides and impurity minerals are still in the grain boundaries, microcracks and crystals, which are difficult to remove. Therefore, long-term acid leaching is used to remove the metal oxides and some silicate minerals soluble in acid. To remove these impurities, the process may be adjusted appropriately based on the ore's characteristics to achieve the desired result, such as using a two-stage pickling process or initial acid leaching. In short, to produce high-purity quartz, every possible method and method should be utilized. Some processes incorporate ultrasonic treatments to ensure the effectiveness of the pickling process.
13. Deionized Water Washing: After acid leaching, the raw material is washed with deionized water to remove any acid and other impurities until neutral.
14. Drying and Packaging: The raw material is dried using specialized drying equipment and vacuum-packed in a cleanroom to produce the finished product.
There are many quartz purification process flows, generally determined by the type, content, and occurrence of impurities in the quartz, as well as product quality requirements. Common quartz purification processes are as follows:
(I) Scrubbing, Classification, and Desliming
During the weathering and sedimentation of quartz sand, a large amount of clay minerals and iron forms cement or adhesion minerals on the quartz surface. Scrubbing, classification, and desliming are commonly used to remove clay impurities, argillaceous iron, and some film-forming iron. For example, the Jiangjin quartzite mine in Sichuan used this process to reduce fine mud and iron to -0.1mm, increasing silica from 85.4% to 97.4% and ferric oxide from 0.63% to 0.165%. This process is generally used as a pretreatment for raw ore before selection, effectively removing argillaceous impurities.
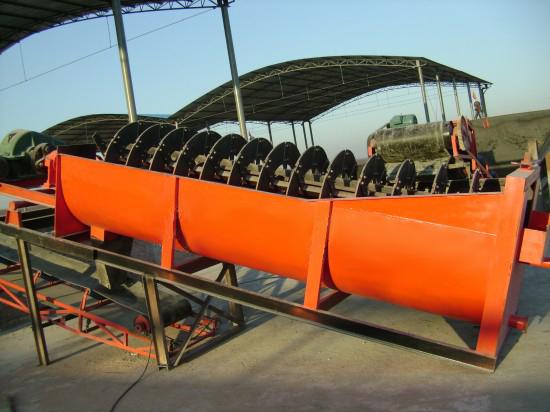
(2) Scrubbing - Desludging - Magnetic Separation
Generally speaking, common impurity minerals in quartz, such as weakly magnetic ores like limonite, tourmaline, hematite, and biotite, and strongly magnetic ores like magnetite, can only be removed through magnetic separation. In actual production, wet high-intensity magnetic separation is often used, with a magnetic field strength of approximately 13,000 Oersteds. After scrubbing and desludging, sedimentary silica sand from Hunan Province contained 0.36% ferric oxide. Purifying this scrubbed and desludged sand using a SHP-500 wet high-intensity magnetic separation machine yielded a ferric oxide content of 0.16%.
(3) Rod Milling - Desliming - Magnetic Separation - Flotation - Acid Leaching
After scrubbing, magnetic separation, and flotation separation, the raw quartz sand ore is essentially free of low-concentration impurity mineral particles (both individual and aggregated). The silica purity generally reaches 99.5%-99.9%, which is sufficient for most industrial applications. However, to further refine it into ultra-high-purity quartz, impurities present as spots and inclusions on the surface of the quartz particles must be acid-leached. Depending on the specific impurity minerals (Fe, Al, Ti, Cr) required for different industrial applications, acid leaching with mixed acids of varying concentrations and ratios is performed. For example, a quartzite ore from Qichun has a silica content of 99.76% and contains fine inclusions. The main impurity minerals, such as Fe, Al, and Ti, exist as clay minerals and iron oxides. After the rod grinding, desliming, magnetic separation, flotation and acid leaching processes, high-purity quartz with a silicon dioxide content of more than 99.99% is obtained.
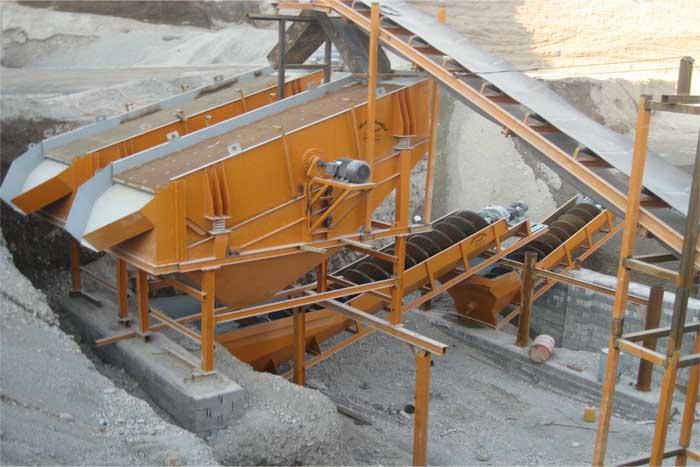
(IV) Chemical Dosing, High-Efficiency, and Powerful Scrubbing – Graded Desliming – Magnetic Separation
After conducting detailed and in-depth experimental research on quartz purification in Yunnan, we pioneered a novel and successful purification process: chemical dosing, high-efficiency, and powerful scrubbing – graded desliming – and magnetic separation. This process improves the structure of existing scrubbing equipment and optimizes technical parameters. Chemical dosing, high-efficiency, and powerful scrubbing, and graded desliming, can remove over 80% of impure iron and aluminum ore. Magnetic separation primarily removes iron-containing impurities. This process produces high-quality refined quartz sand with a silica content of ≥99.8%, ferric oxide ≤0.023%, aluminum oxide ≤0.05%, and titanium dioxide ≤0.02%, meeting the requirements for first-grade optical glass sand. The refined sand yield reaches 73%, compared to only 49% for rod mill scrubbing, and the silica recovery rate is 72.8%. After further reselection and acid leaching treatment, high-purity quartz with silicon dioxide ≥99.9%, iron oxide ≤0.005%, aluminum oxide ≤0.05%, and titanium dioxide ≤0.02% can be obtained. The adoption of this process overcomes the shortcomings of secondary iron pollution caused by rod grinding and scrubbing and low yield.
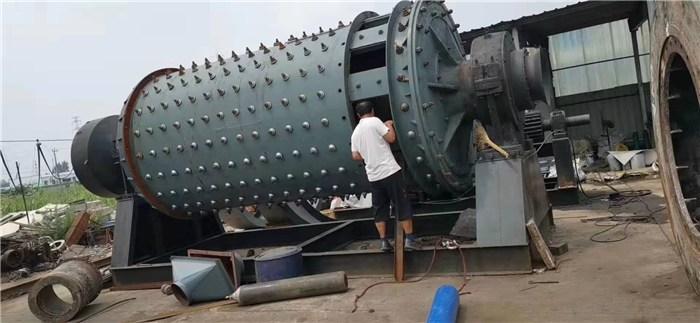
The quartz purification process involves a complex separation technique that removes small or trace impurities from quartz to produce refined quartz sand or high-purity quartz. In recent years, research on quartz purification processes has focused primarily on the following aspects:
(I) Quartz Purification Process - Water Washing, Grading, and Desliming:
The SiO2 grade in quartz decreases as the quartz particle size decreases, while the grade of impurity minerals such as iron and aluminum decreases. This phenomenon is particularly pronounced in quartz containing a high concentration of clay minerals. Therefore, water separation and desliming of the quartz ore before selection are essential and highly effective. For example, the chemical composition of quartz ore from the Malingshan Mine in Suqian, Jiangsu Province is: SiO2 79.38%, Fe2O3 1.68%, and Al2O3 11.28%. The -0.1mm fraction accounts for 27.65% of the particle size. After pre-selection, water washing, and graded desliming of the raw ore, the SiO2 grade rose to 86.36%, Fe2O3 decreased to 0.49%, and Al2O3 decreased to 6.79%, achieving significant impurity removal and purification results. Water washing and graded desliming are a common and early pretreatment method for ore selection, but their removal effect on thin-film iron and adhesive impurity minerals present on the quartz surface is not yet significant.
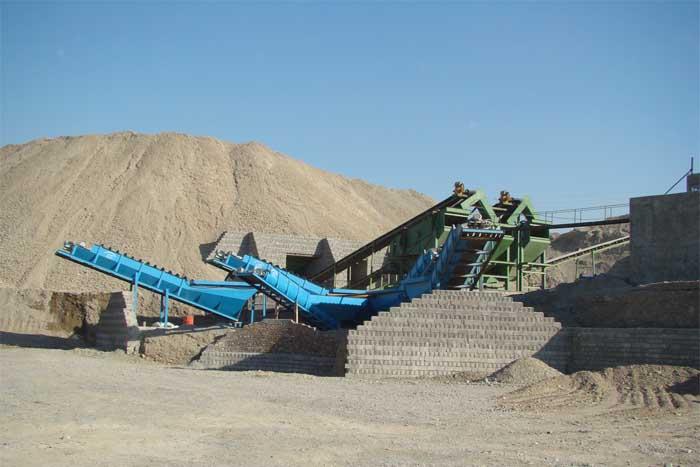
(II) Quartz Stone Purification Process - Scrubbing Purification Process:
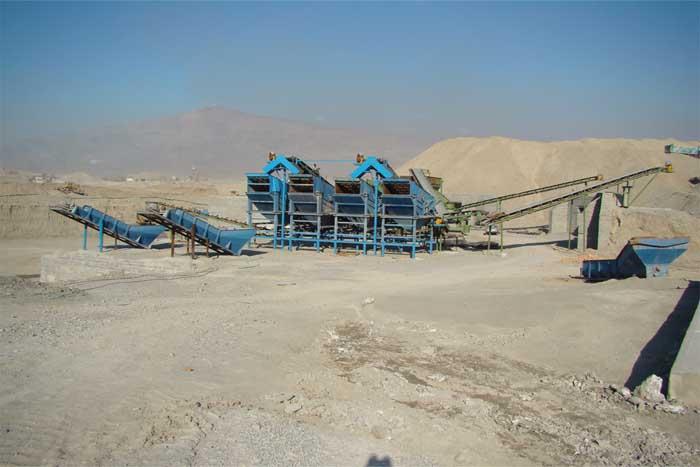
Scrubbing utilizes mechanical force and the abrasive forces between sand grains to remove thin film iron, adhesive and clay impurities from the surface of quartz sand, and further break up unorganized mineral aggregates. Classification is then performed to further purify the quartz sand. Currently, there are two main methods: rod scrubbing and mechanical scrubbing. For mechanical scrubbing, the main factors affecting scrubbing effectiveness are the scrubbing machine's structural characteristics and configuration, followed by process factors, including scrubbing time and scrubbing concentration. Research has shown that a scrubbing concentration of 50%-60% is most effective for sand ore, and to a certain extent, it increases the difficulty of quartz purification. Scrubbing time should generally be based on achieving initial product quality requirements and should not be too long. This can increase equipment wear, energy consumption, and the cost of mineral processing and purification. Because mechanical scrubbing is less effective for some quartz ores, rod scrubbing is more common and relatively mature in my country's industrial applications. For example, after washing, grading, and desludging quartz ore from a certain location, rod milling with quartz sand larger than 0.3 mm was performed. The results showed that after grinding and scrubbing, the Fe₂O₃ content decreased from 0.19% to 0.10%, and the iron removal rate reached 47.4%. We also used high-efficiency, high-power scrubbing with the addition of chemicals on quartz from a location in Yunnan, combining appropriate processes and equipment. The results were superior to rod milling, with a recovery rate of 49% after rod milling, compared to 73% with the addition of chemicals. The purpose of adding chemicals is to increase the electrical repulsion between the impurity minerals and the quartz particles, enhancing the separation between them.
(III) Quartz Purification Process - Magnetic Separation Process:
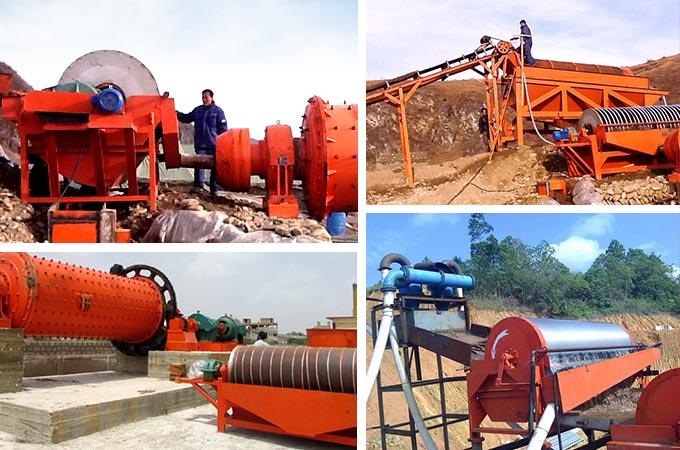
Magnetic separation can maximize the removal of weakly magnetic impurities, including conjoined particles, such as hematite, limonite, and biotite. High-intensity magnetic separation typically utilizes a wet high-intensity magnetic separator or a high-gradient magnetic separator. Generally speaking, quartz impurities primarily composed of weakly magnetic impurities such as limonite, hematite, and biotite can be separated using a wet high-intensity magnetic separator at a force of 10,000 Oersted or higher. For strongly magnetic minerals primarily composed of magnetite, a low-intensity or medium-intensity magnetic separator is more effective. Hiroshi Uemura and Heiji Tabuchi conducted experimental studies on Seto quartz sand using a high-intensity magnetic separator. The results showed that the number of magnetic separations and the intensity of the magnetic field significantly influence the iron removal efficiency. As the number of magnetic separations increases, the iron content gradually decreases. While a certain magnetic field intensity can remove most of the iron, even with significantly higher magnetic field intensity, the iron removal rate remains largely unchanged. In addition, the finer the quartz sand particle size, the better the iron removal effect. The reason is that fine-grained quartz sand contains a high amount of iron impurity minerals. When the raw quartz sand contains a lot of impurity minerals, it is not possible to purify the quartz sand into high-purity sand by only scrubbing, desludging and magnetic separation. In order to further improve the purity of quartz and reduce impurities,
(IV) Quartz Purification Process - Flotation Purification Process:
Considering the serious environmental impact of fluoride-containing wastewater, the "fluoride-free acid flotation method" emerged in the 1970s. For example, Japan has successfully separated feldspar from quartz by using sulfuric acid or hydrochloric acid (pH = 2) to prepare a slurry and flotation with a mixed collector of higher-grade aliphatic amine salts and sodium petroleum sulfonate. Fluoride-free and acid-free flotation is a new flotation separation process for quartz and feldspar that has been vigorously developed in recent years. Tang Jiaying et al. began researching a new flotation separation process using mixed anion and cation collectors in 1984. This method utilizes the structural differences between quartz and feldspar in a naturally neutral medium, rationally adjusting the ratio of anion and cation collectors to preferentially separate the feldspar from the feldspar. However, fluorine-free and acid-free flotation methods are less mature than HF and acid methods, and there are currently no reports of their industrial application. Mica and quartz have similar isoelectric points, making separation difficult. Flotation using anionic collectors under acidic conditions, or anionic-cationic collectors under alkaline conditions, can achieve excellent results. Generally speaking, after scrubbing, desludging, magnetic separation, and flotation, the purity of quartz can reach 99.3%-99.9%, essentially meeting the demand for industrial sand.
(V) Quartz Purification Process - Acid Leaching Process:
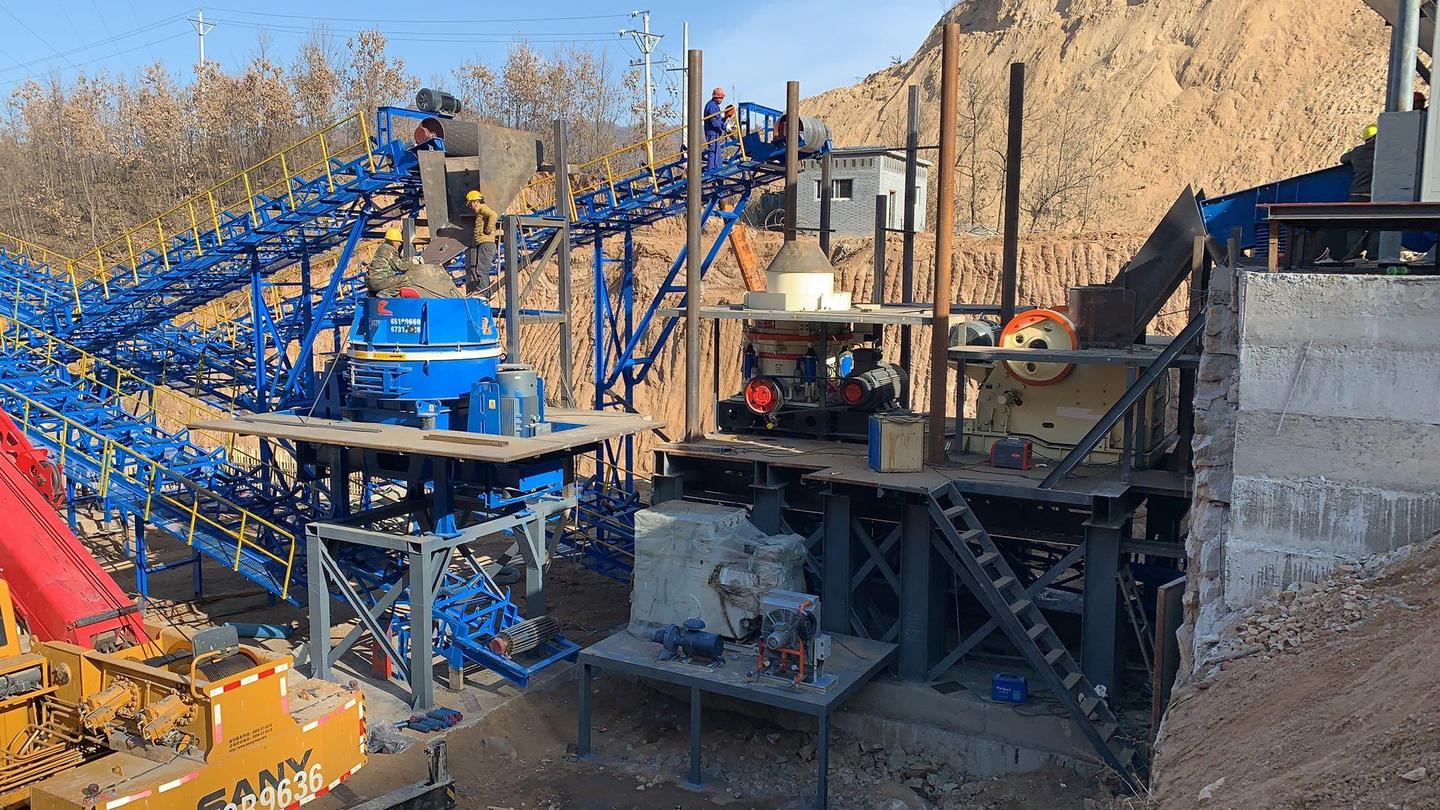
Acid leaching utilizes the fact that quartz is insoluble in acid (except HF), while other impurity minerals can be dissolved by acid, thereby further purifying quartz. Commonly used acids for acid leaching include sulfuric acid, hydrochloric acid, nitric acid, and hydrofluoric acid; reducing agents include sulfurous acid and its salts. Research has found that these acids are effective in removing non-metallic impurities from quartz. However, the type and concentration of acid significantly influence the removal of different metallic impurities. It is generally believed that various dilute acids are effective in removing Fe and Al, while Ti and Cr are most effectively removed by acid leaching with more concentrated sulfuric acid, aqua regia, or HF. A mixture of these acids is typically used for acid leaching to remove impurity minerals. Due to the dissolution of HF on quartz, the HF concentration is generally not allowed to exceed 10%. In addition to the acid concentration, the acid dosage, leaching time, temperature, and slurry agitation can also affect the quartz acid leaching effect. Controlling various factors during acid leaching should be based on the desired final quartz grade. Minimizing acid concentration, temperature, and dosage, as well as reducing leaching time, allows for quartz purification at lower beneficiation costs. Due to stringent requirements for iron in quartz, some European and American countries have systematically studied quartz acid leaching and purification processes, and established acid leaching quartz beneficiation and purification plants. Quartz treated with acid leaching can achieve high-purity quartz with a purity of up to 99.99%.
(VI) Quartz Purification Process - Microbial Leaching Process:
Using microorganisms to remove thin-film iron or impregnated iron from the surface of quartz particles is a recently developed iron removal technology. Research results from abroad have shown that using microorganisms such as Aspergillus niger, Penicillium, Pseudomonas, Polymyxin, and Bacillus to remove thin-film iron from quartz surfaces has achieved excellent results. Aspergillus niger is the most effective for iron removal, with Fe₂O₃ removal rates often exceeding 75%, and concentrate Fe₂O₃ grades as low as 0.007%. Furthermore, it has been found that using pre-cultivated cultures of most bacteria and molds is more effective in leaching iron. This is due to the effects of their soluble metabolites, as with other bacterial species. Currently, microbial iron removal is in the laboratory research stage, and large-scale industrial production requires further experimental research.
(VII) Quartz Purification Process - Other Purification Processes:
Due to the varying requirements for impurity mineral content in different quartz products, other purification methods are sometimes employed for further purification. For example, electrostatic separation utilizes the slight electrical difference between quartz and impurity minerals to select trace amounts of metallic impurities. Thermal chlorination removes gaseous and liquid impurities in quartz, as well as surface contamination from impurity minerals and metal inclusions, further purifying the quartz sand.
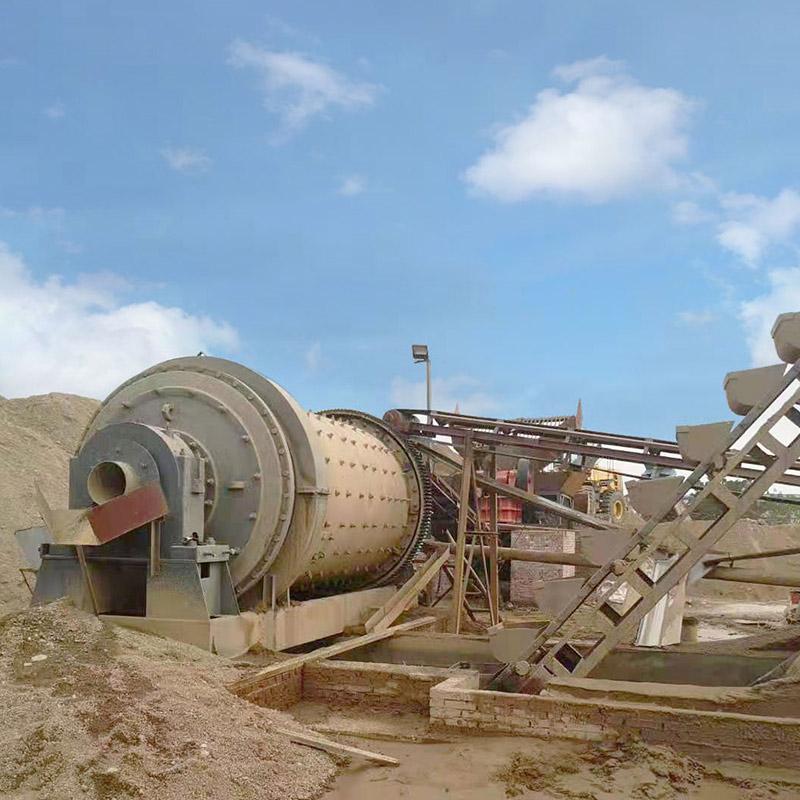
The quartz stone purification process can be divided into two types: wet purification and dry purification. Impurities, particularly iron, are removed from the quartzite ore through mechanical scrubbing combined with magnetic separation, flotation, and acid leaching.
1. Quartz Stone Purification Process - Wet Purification Process: Ore crushing → Stone wheel grinding → Water rinsing → Magnetic separation → Hydraulic classification → Quartz sand concentrate. The wet process primarily produces 20-120 mesh wet sand, which is then acid-washed and flotated to produce 60-140 mesh refined quartz sand.
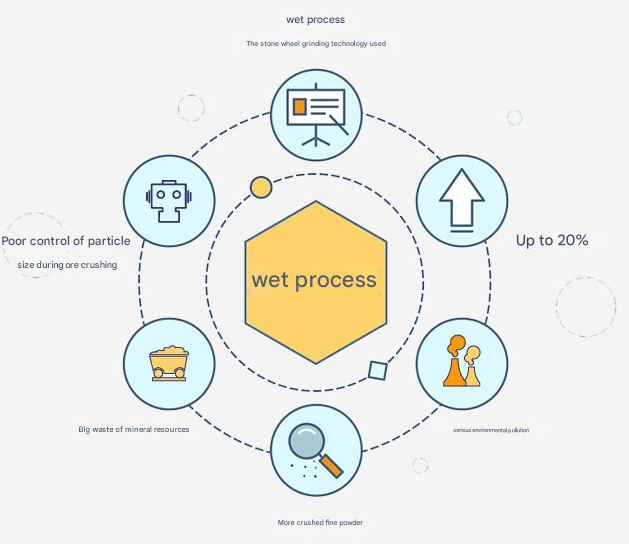
2. Quartz Purification Process - Dry Purification Process: The ore undergoes coarse crushing in a jaw crusher, secondary crushing, screening to remove dirt, grinding in a rod mill, magnetic separation, coarse separation, fine separation, and finally a cyclone. The coarse and fine separations produce silica sand with a mesh size of 20-120. The dry process product undergoes flotation to produce by-products such as 120-mesh fiber sand.
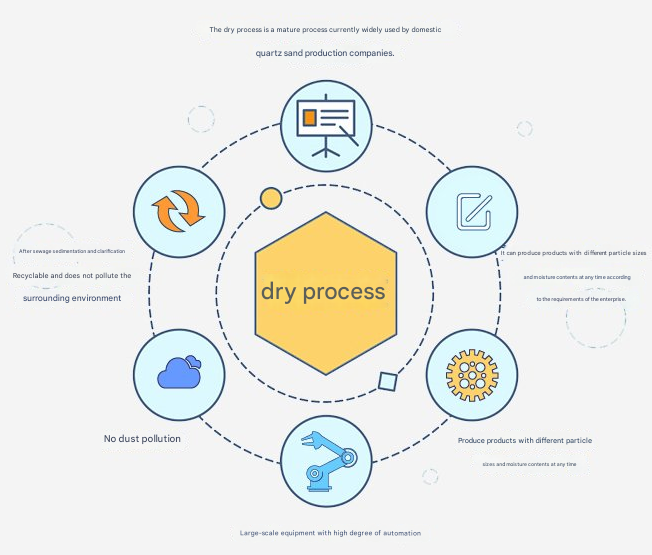
3. Comparative Study of Quartz Stone Purification Processes:
The core of the wet process is the traditional mechanical scrubbing and iron removal technology using stone wheel grinding, combined with magnetic separation, to remove iron impurities from the quartzite ore. The dry process uses a new rod grinding and iron removal technology, combined with magnetic separation, to remove iron impurities from the quartzite ore.
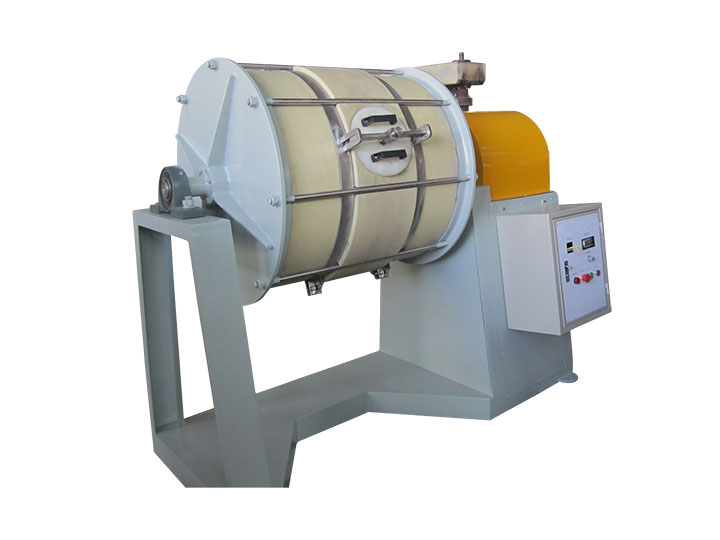
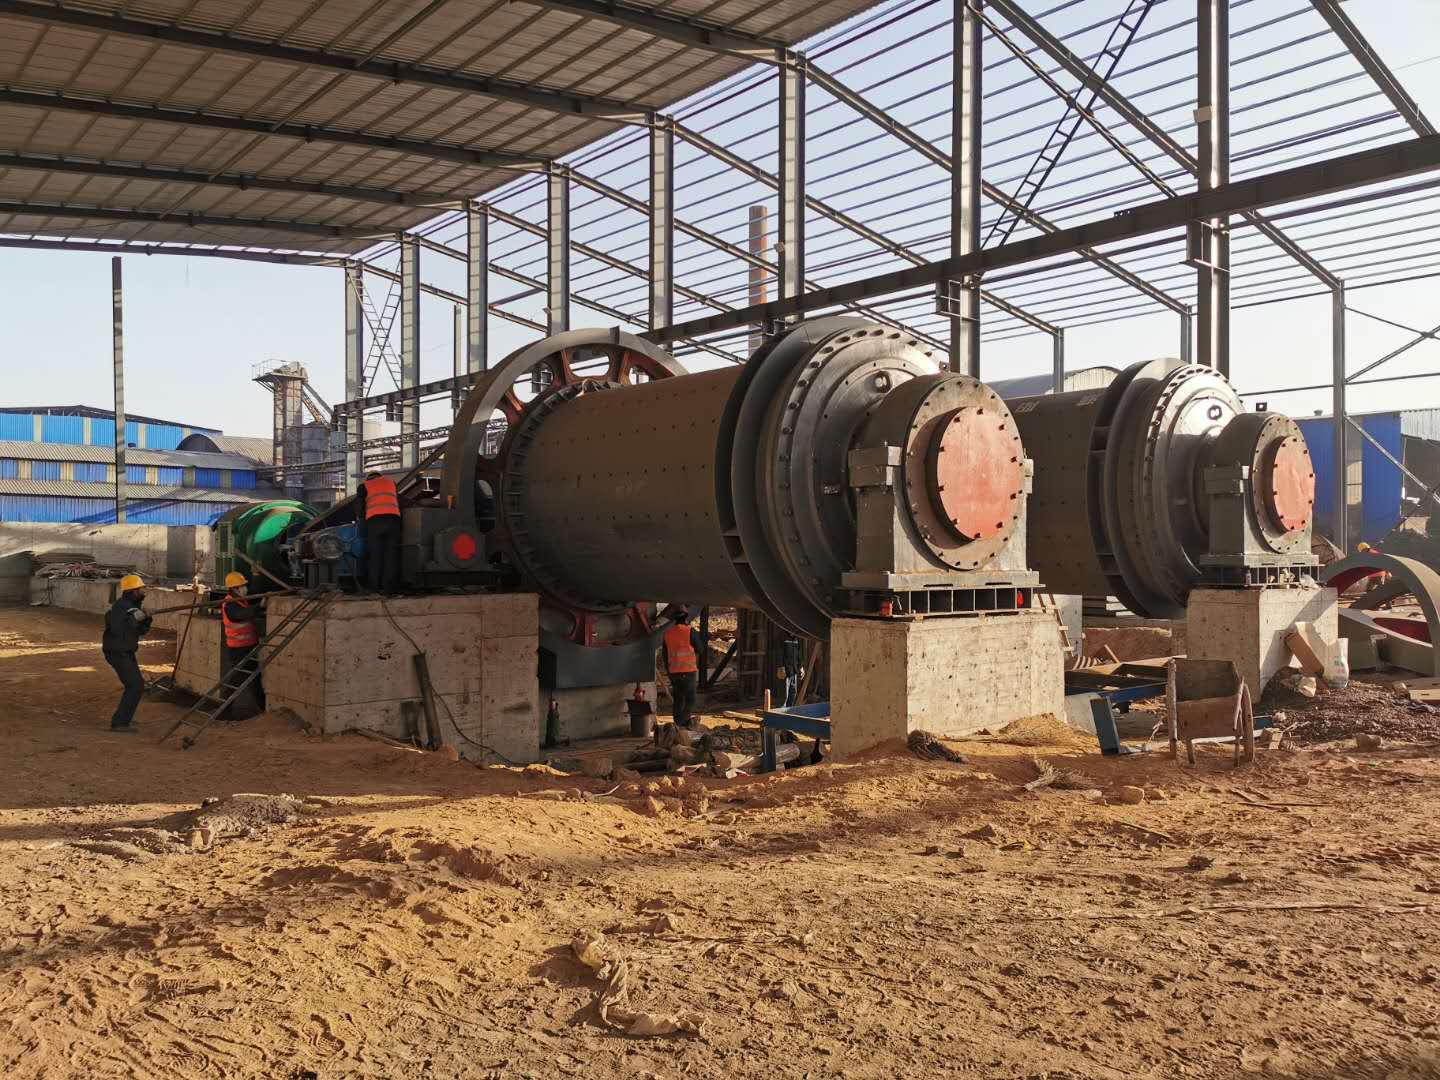
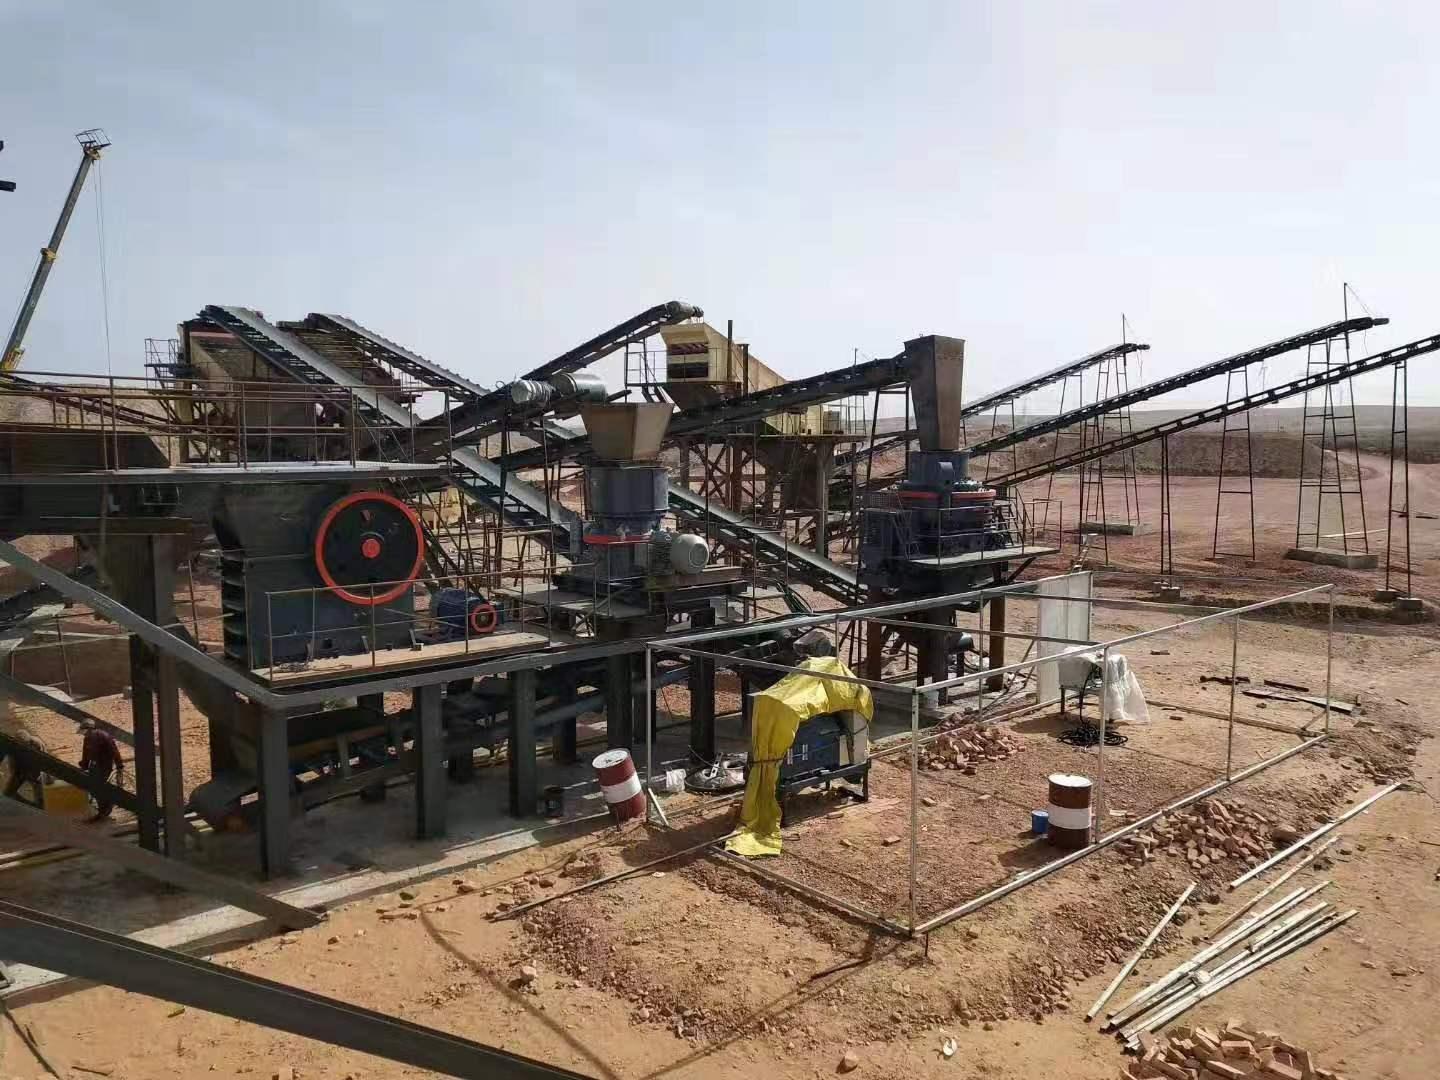
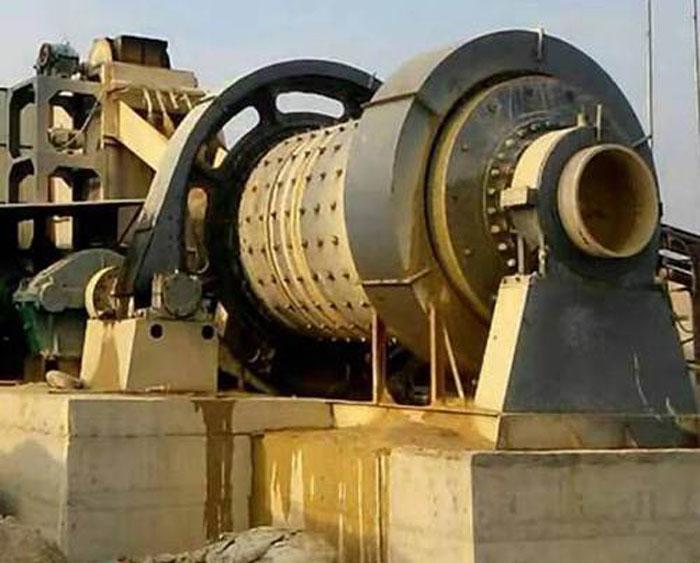
Quartz Stone Purification Process: The main production equipment in the wet quartz sand production line includes jaw crushers, cone crushers (or fine jaw crushers, or impact crushers), quartz sand making machines, quartz rod mills, quartz magnetic separators, quartz flotation machines, sand washers, and dryers. The process generally involves coarse and fine crushing of the quartz stone until it is sanded. The sand is then washed in a sand washer, dried in a dryer, and screened with a vibrating screen. Iron removal is also performed during the screening process. Wet quartz sand production maximizes the cleanliness of the refined quartz sand, resulting in high quality and, therefore, a higher price.
The quartz purification process is generally determined by the following factors: a) the presence of impurity minerals in the raw sand; b) the beneficiation cost of the purification process; and c) the industrial application of the refined sand product. For refined sand quartz intended for general industrial use, a simple quartz purification process is preferred to reduce purification costs. A scrubbing-desludging-magnetic separation process is recommended to meet high-quality requirements. For high-purity and ultra-high-purity quartz intended for high-tech applications, further purification is required through flotation and acid leaching. The quality requirements for high-purity and ultra-high-purity quartz are generally ≥99.99% silicon dioxide and a mass fraction of less than 1×10⁻⁵ iron oxide. The purification process requires not only strict control of separation conditions but also stringent requirements for the corresponding purification equipment to prevent secondary contamination. We pioneered a new quartz stone purification process: high-efficiency, powerful scrubbing with added chemicals, followed by classification and magnetic separation. We successfully purified quartz sandstone from a location in Yunnan, overcoming the drawbacks of rod mill scrubbing, such as secondary iron contamination and low yield. This process is highly significant for achieving low-cost, efficient purification and impurity removal of quartz.
The most advanced quartz stone purification process in the United States is characterized by large industrial production volumes, specialized equipment, and a high degree of production automation. Its products have reached the sixth generation (with a total impurity mass fraction of less than 8×10⁻⁶ and optical-grade transparency). High-purity and ultra-high-purity quartz sand produced through mineral processing and purification is widely used in high-tech fields such as aerospace, atomic energy, lasers, optical fiber communications, and military applications. With technological advancements, the demand for silicon for high-tech applications is expected to increase significantly. However, the increasing depletion of natural crystal resources has necessitated a shift to alternatives to natural crystal—high-purity and ultra-high-purity quartz. Therefore, actively exploring and promoting advancements in quartz mineral processing and purification technology to achieve cost-effective, large-scale industrial production of refined, high-purity, and ultra-high-purity quartz is of great practical significance in offsetting the shortage of natural crystal resources and meeting the demand for silicon for high-tech applications.